Reliable versatility for every threading challenge
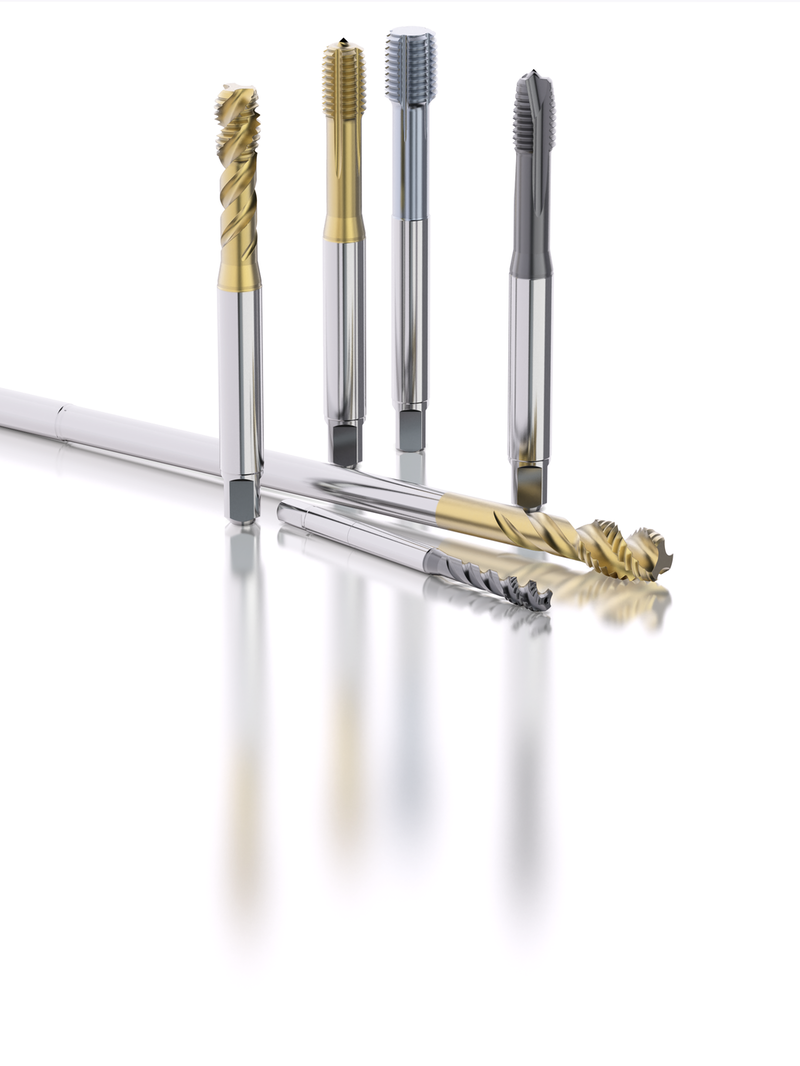
T30 and T35 taps deliver reliable, predictable threading across mixed materials and high‑volume runsT30 and T35 taps support manufacturers in handling everything from high‑mix, low‑volume production to demanding high‑volume runs. Together, they cover a broad material range and deliver consistent, predictable threading performance. T30 provides universal versatility for shops running a wide variety of materials, while the T35 family offers targeted, high‑efficiency solutions optimized for specific material groups including alloyed steels, cast iron, aluminum, and tough/abrasive materials.
T30 for a universal performance in small batches and mixed materials
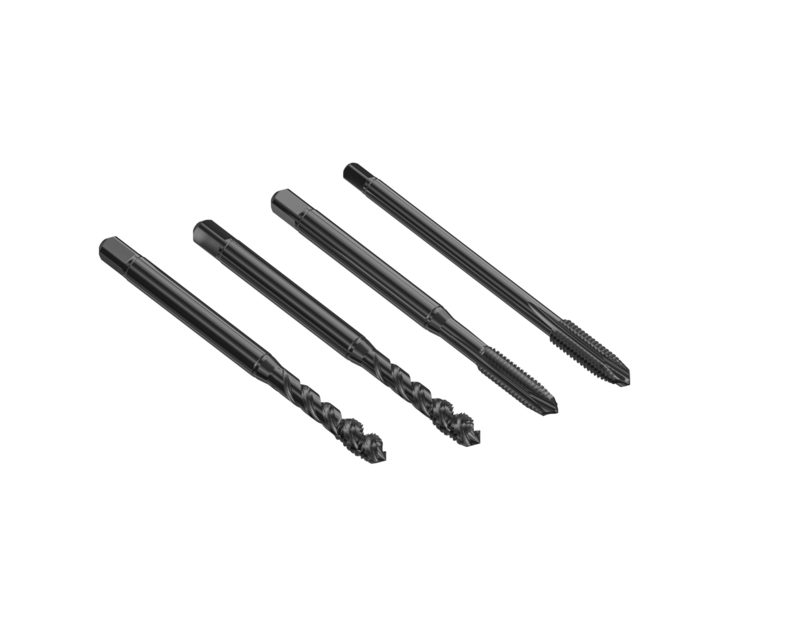
The T30 tapping tool uses a universal geometry engineered to perform across a wide range of materials, helping you to avoid carrying large inventories of rarely used tools. This improves agility and cuts tooling costs, especially in high‑mix, low‑volume environments.
Your challenge: You need tapping tools that can adapt to diverse materials without building a costly, overstocked tool inventory.
Our solution: T30 taps deliver broad material compatibility and consistent performance, getting rid of the need for multiple specialty taps.
Increase agility in high‑mix, low‑volume environments
With a versatile geometry, steam‑oxide options for sticky materials, and an edge preparation that’s designed for dependable chip control, T30 ensures repeatable results even when every job looks different.
Your challenge: Maintaining productivity when every set-up, job, and material changes daily.
Our solution: T30’s universal construction provides dependable performance in steels, stainless steel, cast iron, and aluminum alloys, keeping your shop adaptable and efficient.
Reduce tool costs while improving process efficiency
Because T30 covers a broad spectrum of applications, it minimizes extra purchases, shortens tool selection time, and helps operators move quickly between jobs. Lower overall tooling costs meet higher shop-floor agility.
Your challenge: Rising tooling costs and wasted time selecting the “right” tap for every part.
Our solution: T30 simplifies your tooling strategy with broad use‑case coverage, faster tool identification, and strong general‑purpose performance.
The T35 family is engineered for top‑tier performance
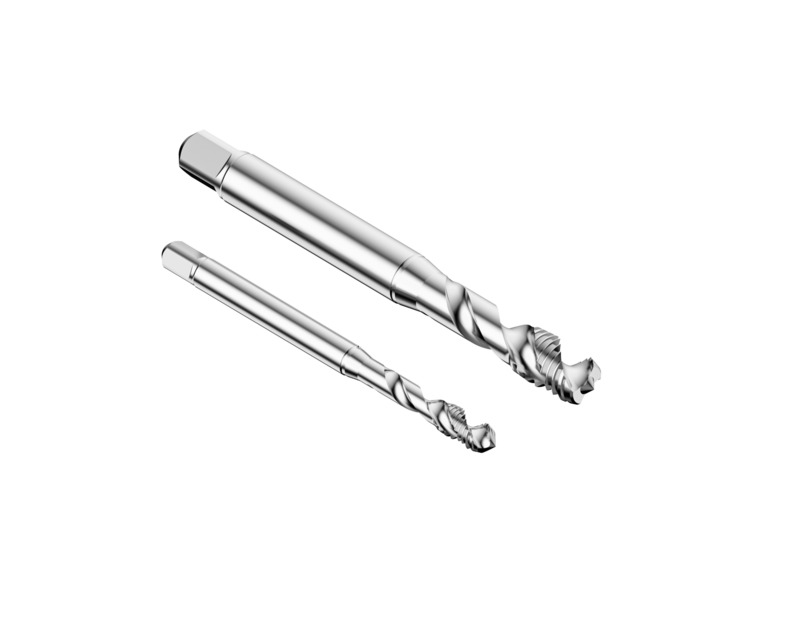
T35‑P for alloyed steels (800–1200 MPa)
T35‑K for abrasive cast iron
T35‑N for aluminum
T35‑H for tough, abrasive materials (30–45 HRC)
Each variant uses specialized geometries and advanced coatings such as TiAlSiN applied via HiPIMS to maximize tool life, thread quality, and process security.
Your challenge: Standard taps wear quickly or fail when used on challenging material types.
Our solution: The T35 series offers purpose‑built geometries matched to steel, cast iron, aluminum, and hard materials which ensures longer tool life and predictable results.
Exceptional tool life and lower part costs
Advanced HSSE‑PM substrates, high‑performance coatings, polished flutes (T35‑N), and optimized flute/chamfer designs deliver superb wear resistance and consistent thread quality in demanding, high‑volume environments.
Your challenge: Tool changes, unpredictable wear, and inconsistent thread quality increase production cost.
Our solution: T35 taps extend tool life and ensure a stable performance, with fewer interruptions and lower scrap rates.
Secure, predictable threading even in difficult materials
The design of the T35 threading tool minimizes miscut threads (especially in cast iron), improves chip evacuation in aluminum, and prevents breakage in tough materials. This reliability boosts confidence in long production runs.
Your challenge: Thread failures, chip blockages, or tool breakage in material‑specific applications.
Our solution: T35 uses geometry tailored to each material to eliminate common tapping issues, whether avoiding miscuts in cast iron or clearing long aluminum chips.
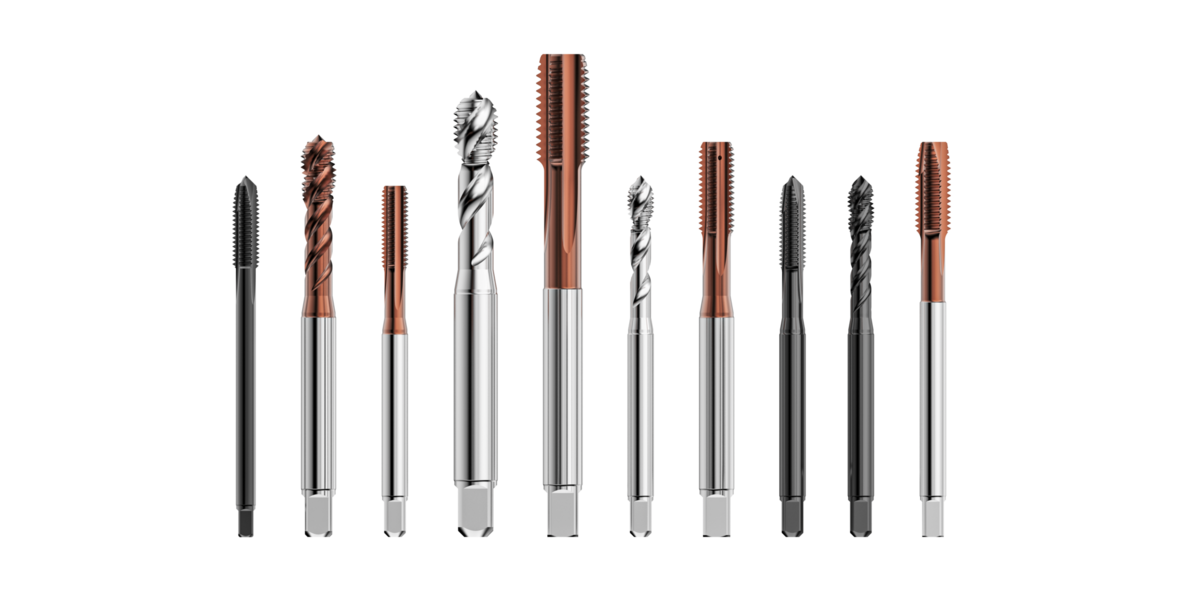
Product ranges - inch and metric taps
T30 range overview
DIN standard (Global)
| Spiral flutes 40°, chamfer C; gunpoint B: | Metric: M3–M52 (steam oxide available) |
| Metric 6G tolerance: M3–M20 |
| Metric fine: M3×0.35 – M48×3 |
| Cylindrical Pipe G: G ⅟₁₆ – G2 |
| UNC: No. 2-56 – 1 ⅜ - 6 |
| UNF: No. 4-48 – 1 ½ - 12 |
|
|
| Straight flutes, chamfer C: | NPT: ½-27 – 1-11 ½ |
| NPTF: ⅛-27 – ½-14 |
| Rc/Rp: Rc ⅟₁₆ –½; Rp ⅛–½ |
DIN/ANSI standard (U.S.)
| Spiral flutes 40°, chamfer C; gunpoint B (steam oxide): | UNC: No. 4-40 – 1-8 |
| UNF: No. 4-48 – 1-12 |
| Metric: M3–M16 |
T35 range overview (combined family)
DIN standard (Global)
| Across P, K, N, H variants: | Metric: M3–M30 |
| Metric fine: MF8×1 – MF20×1.5 |
|
|
| T35-P: Spiral flutes 40°, chamfer C; gunpoint B |
| T35-H: Spiral flutes 15°, chamfer C; gun point B; Straight flutes, chamfer C, internal coolant options |
| T35-K: Straight flutes, chamfer C/E, internal coolant options |
| T35-N: Spiral flutes 45°, chamfer C |
DIN/ANSI standard (U.S.)
| Across P, K, N, H variants: | UNC: No. 4-40 – 1-8 |
| UNF: No. 4-48 – 1-12 |
| Metric: M3–M20 |
| Material specific geometries: | T35-P: Spiral flutes 40°, chamfer C; |
| T35-H: Spiral flutes 15°, chamfer C or E; gun point B; internal coolant options |
| T35-K: Straight flutes, chamfer C |
| T35-N: Spiral flutes 45°, chamfer C |
Click here for your printable summary